显示标签为“steel coil”的博文。显示所有博文

2016年6月27日星期一

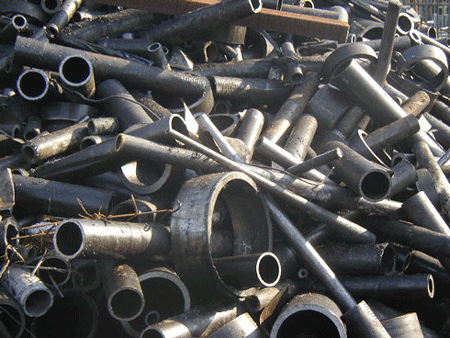
[ News ]Steel scrap: A world-traded commodity


To most, the word ‘scrap’ evokes visions of unwanted, discarded leftovers. However, to the steel industry, scrap represents a vital resource that enhances all aspects of steelmaking.
The recycling of scrap metal is an integral part of modern steelmaking, improving the industry's economic viability and reducing environmental impact. The recycling of steel scrap reduces the need for iron ore extraction, significantly reducing CO2 emissions, energy and water consumption and air pollution.
As a result of these efficiencies, steel scrap is increasingly being regarded as a raw material for manufacturing new products worldwide. Ferrous scrap – iron and steel – has become a globally traded commodity. The increased demand for steel scrap is reflected in recent trade statistics.
The United Nations Commodity Trade Statistics Database shows that the volume of global scrap exports increased from 9.3 million tonnes in 1990 to 106 million tonnes in 2011. Figures from the Bureau of International Recycling show that total world steel scrap use increased 7.6% in 2011 to reach 570 million tonnes.
The globalization of the ferrous scrap market, however, also places stresses on the system. The long lifespan of steel products means that the amount of steel available for recycling cannot keep up with the current world demand for new steel products. With steel, structures can last longer than 60 years and cars often last longer than 12 years; steel products can be seen as scrap-in-inventory – meaning that the steel will not be ready for recycling until the long life of the product comes to an end.
A positive aspect of steel is the ease of recycling when products finally do reach the end of their life. The ability to recover and collect old steel products for subsequent recycling is greatly enhanced by the inherent magnetic properties of steel; consequently, a large tonnage of steel becomes available for recycling every year.
Figures from the US Census Bureau and the US International Trade Commission demonstrate that the US is the world’s largest exporter of ferrous scrap – exporting nearly 23 million tonnes of iron and steel scrap in 2011. Globally, China, Taiwan, South Korea, India, Canada, and Turkey are the largest markets for exports of US steel scrap in that same period.
Ferrous scrap exports from the EU to third countries reached a record high in 2012. The 27 member states exported around 19.22 million tonnes of iron and steel wastes and scrap valued at €6.8 billion to countries outside the Union (extra-EU trade), according to preliminary figures released by the European Statistical Office, Eurostat. The export volume exceeded the 2011 amount of 18.81 million tonnes by 407,000 tonnes or 2.2%. The UK was by far the largest exporter of the EU-27, shipping nearly 5.2 million tonnes of ferrous scrap outside the EU. The most important destination country for EU ferrous scrap was Turkey. At 11.05 million tonnes and a value of €3.3bn, around 58% of all extra-EU ferrous scrap exports headed to this country (2011: 9.97 million tonnes, €3.1bn).
North America is also one of the largest consumers of its own steel scrap – recycling more than 70% of that scrap domestically, with mini-mills being the primary source of recycled steel. Mini-mills use electric arc furnaces, which melt scrap metal via the heat produced by an electric arc. US producers Nucor (one of the world's largest steel producers), as well as one of its competitors, Commercial Metals Company (CMC) use mini-mills exclusively. Since the electric arc furnace can be easily started and stopped on a regular basis, mini-mills can follow the market demand for their products easily, operating on 24 hour schedules when demand is high and cutting back production when sales are lower.
“This high level of scrap consumption is a reflection of the steel industry’s commitment to conserving energy and natural resources,” said Gregory Crawford, executive director of the Steel Recycling Institute in North America. “Scrap steel is used in everyday products, including packaging, appliances, automobiles and construction. Each year, more steel is recycled in North America than paper, aluminum, plastic and glass combined.”
This flow of scrap also faces challenges in the form of trade restrictions. The Organization for Economic Cooperation and Development (OECD) reported in 2012 that North American and European ferrous scrap is traded openly, but that about 19 percent of the scrap trade is burdened by various trade restrictions.
The 2012 OECD report noted that “waste and scrap exports are restricted in many parts of the world. Waste and scrap trade involving iron and steel and non-ferrous base metals (copper, aluminum, lead and zinc) tends to be more regulated than trade involving other metals.”
The OECD found that, in 2009, at least 19% of scrap of iron and steel, exported by a total of 34 countries, was subject to export restrictions. “Export restrictions dampen trade flows,” stated the report. “In fact, some exports actually will not take place due to the very fact that export restrictions are in place. Export activity would be higher if restrictions did not exist.”
The rationales that governments cite most frequently as motivating their use of the restrictions include safeguarding domestic supplies, controlling illegal exports, and protecting local industry. Non-automatic export licensing, export taxes and other export prohibitions were among the measures used to regulate the export of iron and steel scrap, according to the OECD.
[ Wiki ] Steel in Buildings and infrastructure


Construction is one of the most important steel-using industries, accounting for more than 50% of world steel production. Buildings - from houses to car-parks to schools and skyscrapers - rely on steel for their strength. Steel is also used on roofs and as cladding for exterior walls.
According to the UN's latest forecast dating July 2015, world population will reach 8.5 billion in 2030 and 9.7 billion in 20501..This will be accompanied by rapid urbanisation. As the need for buildings and infrastructure continues to grow worldwide, reducing consumption of natural resources and associated emissions is crucial for future sustainability.
Steelmakers around the world are increasingly providing construction solutions that enable energy-efficient and low-carbon-neutral buildings. These solutions reduce the environmental impact over the structures’ life cycle and help to extend their life span through design for disassembly and reuse.
Steel can provide the solutions to infrastructure and construction needs in developing countries and in climate resilient cities through enabling protective coastal and wind-resistant designs. While buildings currently account for about 20% of global greenhouse gas emissions, they also present many opportunities for reducing emissions and mitigating climate change.2,3
Not only is steel affordable, readily available and safer, its intrinsic properties, such as strength, versatility, durability and 100% recyclability allow for improved environmental performance across the entire life cycle of buildings. 
The advanced high-strength steels used in steel-plate applications also find uses in a number of related industries. Offshore oil rigs, bridges, civil engineering and construction machines, rail carriages, tanks and pressure vessels, nuclear, thermal and hydroelectric plants – all these applications benefit from the attributes of modern steels.
How steel is used in buildings and infrastructure
The possibilities for using steel in buildings and infrastructure are limitless. The most common applications are listed below4.

For buildings

  • Structural sections: these provide a strong, stiff frame for the building and make up 25% of the steel use in buildings.
  • Reinforcing bars: these add tensile strength and stiffness to concrete and make up 44% of steel use in buildings. Steel is used because it binds well to concrete, has a similar thermal expansion coefficient and is strong and relatively cost-effective. Reinforced concrete is also used to provide deep foundations and basements and is currently the world’s primary building material.
  • Sheet products: 31% is in sheet products such as roofing, purlins, internal walls, ceilings, cladding, and insulating panels for exterior walls.
  • Non-structural steel: steel is also found in many non-structural applications in buildings, such as heating and cooling equipment and interior ducting.
  • Internal fixtures and fittings such as rails, shelving and stairs are also made of steel. 

For infrastructure


[ Wiki ]What surface finishes are available/application do i choose on stainless steels?

What surface finishes are available on stainless steels?


There are many different types of surface finish on stainless steel. Some of these originate from the mill but many are applied later during processing, for example polished, brushed, blasted, etched and coloured finishes.
The importance of surface finish in determining the corrosion resistance of the stainless steel surface cannot be overemphasised. A rough surface finish can effectively lower the corrosion resistance to that of a lower grade of stainless steel.
The European standards for stainless steels have attempted to define the most common surface finishes. However, due to the proprietary nature of many suppliers’ finishes, it is unlikely that complete standardisation is possible. This is a summary of the most common types for each product form
Common Surface Finishes for Flat Products from EN 10088-2 (for full list see Specifying finishes for stainless steel flat products (sheet and plate)
Surface Finish Code
Description
Mill finishes
 
1D
Hot rolled, heat treated, pickled. The most common hot rolled finish. A non reflective, rough surface. Not normally used for decorative applications
2B
Cold rolled, heat treated, pickled, pinch passed. The most common cold rolled mill finish. Dull grey slightly reflective finish. Can be used in this condition or frequently is the starting point for a wide range of polished finishes.
2D
Cold rolled, heat treated, pickled.
2H
Work hardened by rolling to give enhanced strength level. Various ranges of tensile or 0.2% proof strength are given in EN 10088-2 up to 1300 MPa and 1100 MPa respectively dependent on grade
2Q
Cold rolled hardened and tempered. Applies to martensitic steels which respond to this kind of heat treatment.
2R
Cold rolled and bright annealed, still commonly known as BA. A bright reflective finish. Can be used in this condition or as the starting point for polishing or other surface treatment processes e.g. colouring

In the following codes “1” refers to hot rolled being the starting point and “2” as cold rolled
Special Finishes
 
1G or 2G
Ground. Relatively coarse surface. Unidirectional. Grade of polishing grit or surface roughness can be specified
1J or 2J
Brushed or dull polished. Smoother than 1G/2G. Grade of polishing grit or surface roughness can be specified
1K or 2K
Satin polish. Similar to 1J/2J but with maximum specified Ra value of 0.5 micron. Usually achieved with SiC polishing belts. Alumina belts are strongly discouraged for this finish as this will have detrimental effect on corrosion resistance. Recommended for external architectural and coastal environments where bright polish (1P/2P) is not acceptable.
1P/2P
Bright polished. Non-directional, reflective. Can specify maximum surface roughness. The best surface for corrosion resistance.
2L
Coloured by chemical process to thicken the passive layer and produce interference colours. A wide range of colours is possible.
1M/2M
Patterned. One surface flat.
1S/2S
Surface coated e.g. with tin = Terne coating
2W
Corrugated. Similar to patterned but both surfaces are affected
Bead blasting
Not in EN 10088-2. Work being undertaken to more accurately define finishes.


How do I choose which stainless steel to use?


Most decisions about which steel to use are based on a combination of the following factors:
  1. What is the corrosive environment? – Atmospheric, water, concentration of particular chemicals, chloride content, presence of acid.
  2. What is the temperature of operation? – High temperatures usually accelerate corrosion rates and therefore indicate a higher grade. Low temperatures will require a tough austenitic steel.
  3. What strength is required? – Higher strength can be obtained from the austenitic, duplex, martensitic and PH steels. Other processes such as welding and forming often influence which of these is most suitable. For example, high strength austenitic steels produced by work hardening would not be suitable where welding was necessary as the process would soften the steel.
  4. What welding will be carried out? - Austenitic steels are generally more weldable than the other types. Ferritic steels are weldable in thin sections. Duplex steels require more care than austenitic steels but are now regarded as fully weldable. Martensitic and PH grades are less weldable.
  5. What degree of forming is required to make the component? – Austenitic steels are the most formable of all the types being able to undergo a high degree of deep drawing or stretch forming. Generally, ferritic steels are not as formable but can still be capable of producing quite intricate shapes. Duplex, martensitic and PH grades are not particularly formable.
  6. What product form is required? – Not all grades are available in all product forms and sizes, for example sheet, bar, tube. In general, the austenitic steels are available in all product forms over a wide range of dimensions. Ferritics are more likely to be in sheet form than bar. For martensitic steels, the reverse is true.
  7. What are the customer’s expectations of the performance of the material? – This is an important consideration often missed in the selection process. Particularly, what are the aesthetic requirements as compared to the structural requirements? Design life is sometimes specified but is very difficult to guarantee.
  8. There may also be special requirements such as non-magnetic properties to take into account.
  9. It must also be borne in mind that steel type alone is not the only factor in material selection. Surface finish is at least as important in many applications, particularly where there is a strong aesthetic component. See Importance of Surface Finish.
  10. Availability. There may be a perfectly correct technical choice of material which cannot be implemented because it is not available in the time required.
  11. Cost. Sometimes the correct technical option is not finally chosen on cost grounds alone. However, it is important to assess cost on the correct basis. Many stainless steel applications are shown to be advantageous on a life cycle cost basis rather than initial cost. See Life Cycle Costing.
The final choice will almost certainly be in the hands of a specialist but their task can be helped by gathering as much information about the above factors. Missing information is sometimes the difference between a successful and unsuccessful application. See also General principles for selection of stainless steels